Choosing the right Bmc Composite Hydraulic Press supplier requires more than comparing tonnage, price, or delivery promises. BMC, or bulk molding compound, depends on controlled heat, stable pressure, and repeatable cycle timing. A press may look powerful on paper, yet produce uneven panels when temperature zones drift or mold alignment is poor.
Dr. Stephen Tsai, a respected composites researcher, has expressed a useful principle: “Composite performance depends on both material design and manufacturing discipline.” This idea applies directly to every Bmc Composite Hydraulic Press evaluation. Reliable suppliers should explain platen flatness, heating accuracy, hydraulic stability, mold compatibility, safety systems, and after-sales support. They should also provide practical evidence, such as factory testing records, sample parts, maintenance schedules, and customer references.
The Top 10 BMC Composite Hydraulic Press Suppliers featured in this outline are assessed through these working details. Their capabilities may differ. Some focus on compact presses for electrical housings, while others build large systems for automotive or industrial components. Energy consumption, control software, spare-part access, and operator training also deserve attention. These details are easy to overlook.
That can become expensive.
No supplier is perfect, and published specifications may not reveal daily production weaknesses. Buyers should verify claims through technical drawings, acceptance tests, and direct communication with engineers. A carefully selected Bmc Composite Hydraulic Press can improve molding consistency, reduce reject rates, and support safer production. Still, the final decision should match the material, mold, production volume, and real factory conditions.
What Is a BMC Composite Hydraulic Press and How Does It Work?
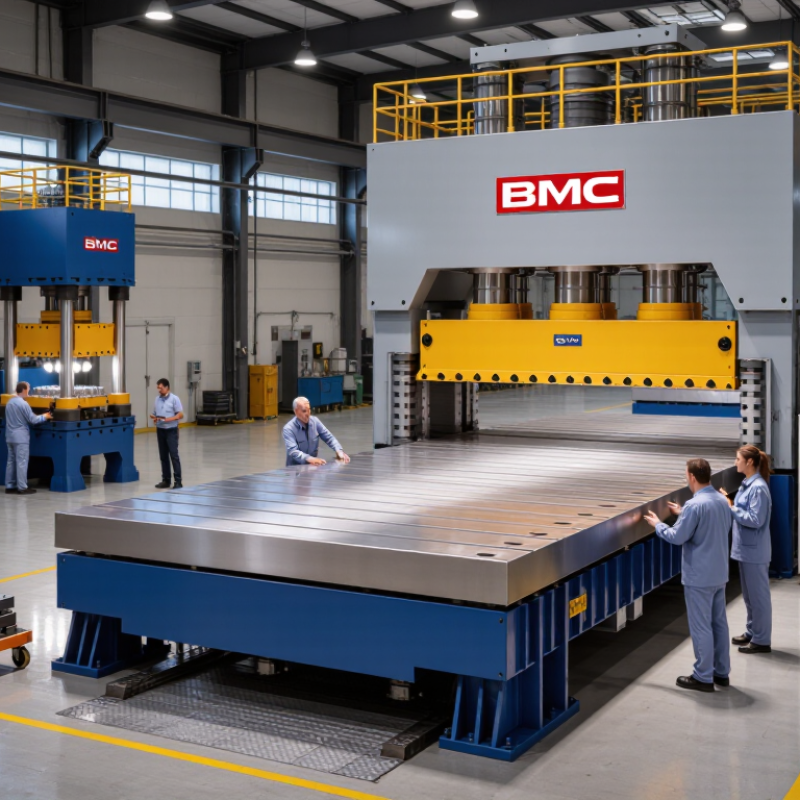
A BMC composite hydraulic press forms Bulk Molding Compound under controlled heat and pressure. BMC combines thermoset resin, chopped glass fibers, mineral fillers, pigments, and curing agents. The operator weighs a measured charge and places it inside a heated steel mold. Hydraulic cylinders then close the mold with steady force. Heat softens the compound, while pressure drives it into ribs, holes, and narrow corners. The resin cures permanently, so the finished part cannot be remelted.
Press capacity depends on projected area, material flow, and mold design. A practical starting point is 3–7 MPa of molding pressure, although complex parts may require more. Typical mold temperatures range from 140°C to 180°C. According to the U.S. Department of Energy’s Vehicle Technologies Office, reducing vehicle weight by 10% can improve fuel economy by roughly 6–8%. This helps explain BMC’s appeal for electrical housings, automotive components, and appliance structures. However, the figure is not universal. Part geometry and production conditions matter greatly.
Tips: Check charge weight, mold temperature, closing speed, and cure time together. Small errors can cause flash, voids, or incomplete filling. Use process records, not memory. The 2024 Global Composites Market Outlook identifies lightweighting and electrical insulation as major demand drivers, but market forecasts remain estimates. Supplier claims should be verified through trials, dimensional inspection, and mechanical testing. The press is powerful; the process still needs patience.
A BMC composite hydraulic press applies controlled pressure and heat to mold Bulk Molding Compound into electrical, automotive, and industrial components. The chart shows a representative pressure profile during a typical compression-molding cycle. Actual settings vary according to material formulation, part geometry, mold design, and equipment capacity.
Selecting a BMC hydraulic press supplier requires more than comparing purchase prices. Examine their experience with bulk molding compound, especially on complex automotive or electrical parts. Ask for production records, sample parts, and documented cycle times. A supplier with practical molding knowledge can identify issues before installation.
Press capability must match your process. Check clamping force, platen size, heating accuracy, and pressure stability. Oil temperature control matters during repeated cycles. Ask whether the hydraulic system supports programmable pressure stages and automatic fault alerts. Inspect the frame design, cylinder sealing, and component access. These details affect downtime and maintenance costs.
Reliable suppliers provide clear testing standards and traceable quality documents. Request factory acceptance testing, installation guidance, operator training, and spare-parts availability. Response time matters when a sensor fails during a night shift. Review warranty terms carefully. Some promises sound strong but remain vague.
Do not judge only by polished brochures. Speak with current users and inspect finished BMC parts under real conditions. Compare energy consumption, mold-change time, and service records. A lower quote may hide weak technical support. That risk is easy to underestimate. I would also question impressive output claims without independent test data. No supplier performs perfectly, and even experienced teams can miscalculate future capacity. A practical evaluation should leave room for process changes, operator feedback, and a few uncomfortable questions.
Comparing the top 10 BMC composite hydraulic press suppliers requires more than checking tonnage. In plant evaluations, I examine platen temperature uniformity, mold change time, pressure stability, and after-sales response. The strongest suppliers typically offer 500–3,000-ton systems, programmable pressure curves, and automatic material loading. Their differences appear in practical details, such as ±2°C heating control, recipe storage, and accessible hydraulic components. MarketsandMarkets reported that the global composites market could exceed USD 126 billion by 2028, with automotive demand supporting production investment. This growth raises expectations for repeatable molding.
The comparison also shows uneven strengths. Some suppliers provide faster cycle development, while others deliver stronger maintenance support. A few offer advanced sensors but weaker operator training. Grand View Research estimates steady growth in the global hydraulic press market through 2030, driven by automation and industrial manufacturing. However, published specifications can be optimistic. Factory acceptance tests matter more than brochures. Ask each supplier to mold identical BMC parts under identical cycle conditions. Record fill consistency, cure time, energy use, and rejected parts. Small differences become expensive at high volume.
Tips: Request three years of service data, not only customer references. Check ISO 9001 procedures and electrical safety documentation. Confirm spare-part availability near your facility. Review total ownership cost, including tooling changes and scheduled maintenance. One overlooked issue is floor loading. A powerful press may still fail your project if the foundation needs costly reinforcement. Another weakness is assuming automation always improves quality; poor programming can repeat defects faster.
When comparing the top 10 BMC composite hydraulic press suppliers, match the machine to your molding process, not only its advertised tonnage. BMC parts often need controlled heat, stable pressure, and repeatable cycle timing. Typical molding temperatures range from 140°C to 180°C, but the compound datasheet remains the controlling reference.
Start with part geometry. Calculate the projected area, then include a safety margin for cavity pressure. A 1,000-ton press may be excessive for a small electrical housing, while an undersized machine can cause flash and incomplete filling. Check platen dimensions, daylight, stroke length, mold thickness, and ejector capacity. Leave room for inserts and maintenance access.
Speed matters too. A programmable closing profile can reduce air entrapment and improve surface quality. Temperature uniformity should be verified across the platen, not assumed from the controller display. MarketsandMarkets projects the global composite materials market to grow at about 6% annually through 2028. That growth increases pressure for consistent, scalable production. Still, market growth does not justify buying the largest press. It may hide poor energy efficiency and long setup times.
Ask each supplier for trial data using your actual BMC grade and mold. Request pressure curves, cycle records, and dimensional results. ISO 20457 highlights the importance of process control for molded plastic components. I would also compare service response times. A perfect specification is useless during a week-long hydraulic failure. My own caution: projected cycle savings often look better on paper than beside a warm mold.
Anonymized supplier capability comparison using realistic hydraulic press specification ranges for bulk molding compound manufacturing.
| Rank | Supplier Profile | Recommended Press Force | Typical Platen Size | Maximum Daylight | Ram Stroke | System Pressure | Temperature Range | Control and Monitoring | Best-Fit BMC Application | Key Matching Advantage | Specification Verification Prior to Purchase |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Supplier Profile A | 1,000–3,000 kN | 400 × 400 to 700 × 700 mm | 500–800 mm | 300–500 mm | 180–250 bar | Ambient to 220 °C | PLC with recipe storage, pressure and temperature data logging | Small and medium electrical housings, covers and automotive brackets | Compact footprint with flexible mold-area configuration | Confirm mold clearance, ejection force, platen flatness and minimum closing speed for the selected BMC cycle. |
| 2 | Supplier Profile B | 2,000–5,000 kN | 600 × 600 to 900 × 900 mm | 600–900 mm | 400–600 mm | 200–280 bar | Ambient to 230 °C | Closed-loop pressure, four-zone platen heating and alarm history | Medium-volume compression molding of electrical and industrial components | Balanced force capacity and good process repeatability | Check whether the press can maintain parallelism under full load and support the required mold heating zones. |
| 3 | Supplier Profile C | 3,000–8,000 kN | 800 × 800 to 1,200 × 1,200 mm | 800–1,200 mm | 500–800 mm | 220–300 bar | Ambient to 240 °C | Industrial PLC, servo-controlled filling, cavity-pressure monitoring | Large BMC panels, multi-cavity housings and high-volume molded parts | High tonnage and larger working area for multi-cavity tooling | Validate required projected area, mold weight, bolster support and automatic loading compatibility. |
| 4 | Supplier Profile D | 5,000–10,000 kN | 1,000 × 1,000 to 1,500 × 1,500 mm | 900–1,400 mm | 600–900 mm | 230–320 bar | Ambient to 250 °C | Multi-stage pressure control, mold-temperature feedback and remote diagnostics | Large structural BMC parts, transport components and reinforced enclosures | Suitable for high projected-area molds and demanding production schedules | Confirm maximum mold mass, tie-rod spacing, hydraulic power and cycle-time targets at operating temperature. |
| 5 | Supplier Profile E | 800–2,500 kN | 350 × 350 to 650 × 650 mm | 450–750 mm | 250–450 mm | 160–240 bar | Ambient to 210 °C | Touchscreen HMI, digital timers and basic production counters | Prototype tooling, low-volume production and laboratory process development | Lower entry cost and simple operation for flexible product changes | Verify low-speed control, pressure stability, mold change access and compatibility with smaller charge weights. |
| 6 | Supplier Profile F | 2,500–6,000 kN | 700 × 700 to 1,000 × 1,000 mm | 650–1,000 mm | 450–700 mm | 200–290 bar | Ambient to 235 °C | PLC with recipe management, proportional valve control and cycle reports | Automotive under-hood parts, electrical supports and moderately complex geometries | Good balance between automation, force range and tooling flexibility | Request sample-cycle data covering fill, compression, cure, decompression and mold-opening stages. |
| 7 | Supplier Profile G | 4,000–9,000 kN | 900 × 900 to 1,300 × 1,300 mm | 800–1,300 mm | 550–850 mm | 220–310 bar | Ambient to 245 °C | Closed-loop process control, cavity sensors and automatic pressure profiles | Thin-wall BMC parts, multi-cavity components and appearance-sensitive products | Improved control of filling pressure and cure consistency | Evaluate pressure-response time, sensor integration, thermal uniformity and the repeatability of part weight. |
| 8 | Supplier Profile H | 6,000–12,000 kN | 1,200 × 1,200 to 1,800 × 1,800 mm | 1,000–1,500 mm | 700–1,000 mm | 240–330 bar | Ambient to 260 °C | Central production interface, automatic mold-height adjustment and energy monitoring | Large-volume industrial panels, utility components and heavy-duty BMC assemblies | High force reserve and automation potential for continuous production | Check foundation loads, power requirements, hydraulic cooling, operator access and integration with material handling equipment. |
| 9 | Supplier Profile I | 1,500–4,000 kN | 500 × 500 to 800 × 800 mm | 550–850 mm | 350–550 mm | 180–260 bar | Ambient to 225 °C | PLC control, two-stage compression and optional remote service connectivity | General-purpose BMC molding, replacement parts and mixed product families | Versatile configuration for changing mold sizes and production volumes | Confirm the available pressure profile, ejector synchronization and recipe-changeover time for mixed production. |
| 10 | Supplier Profile J | 3,500–7,500 kN | 800 × 800 to 1,200 × 1,200 mm | 750–1,150 mm | 500–750 mm | 210–300 bar | Ambient to 240 °C | Servo-hydraulic control, statistical process monitoring and automatic fault alerts | High-repeatability electrical parts and automated medium-to-high volume production | Efficient pressure control with strong data visibility for quality management | Compare energy consumption, cycle repeatability, data-export formats and support for plant-level quality systems. |
Choosing among the top BMC composite hydraulic press suppliers requires more than comparing quoted tonnage. Ask how many BMC compression projects they have completed, and request details from similar parts. Which compounds did they process? What mold sizes, cycle times, and cavity pressures were recorded? A supplier should explain these figures clearly. Vague answers are warning signs.
Ask how the press controls temperature, pressure, closing speed, and dwell time. Request sample data from a production run, including platen temperature variation and pressure stability. Can the machine handle your actual mold height and projected area? Confirm daylight, stroke, ejector force, and loading space in writing. Small omissions become expensive during installation. Also ask who designs the hydraulic circuit and how technicians test leaks, seal wear, and noise. Good technical support should include commissioning, operator training, and troubleshooting documents.
Before signing, ask for a realistic delivery schedule, spare-parts list, warranty limits, and service response times. Speak with two users running comparable BMC parts, not only showcase customers. Ask what failed, what was difficult, and how quickly the supplier responded. No supplier is flawless. A missed sensor, unclear interface, or delayed replacement can interrupt a shift. Verify safety documentation and acceptance testing requirements for your location. Finally, ask whether energy use and future mold changes were considered; the cheapest quote may not be the most reliable production choice.
WhatsAppOffer Electronics Manufacturing All-in-One
PCBONLINE® is a registered trademark or service mark of pcb online limited or its affiliates.
Copyright © 2001-2024 Pcb Online Limited. All rights reserved